


- Services & Equipment
- /
- Process Equipment
Flotation Technologies
Advanced flotation solutions for efficient mineral recovery and optimised processing performance.


Contact Information
"*" indicates required fields

Get the
full technical overview
- Overview
Optimised Mineral Recovery
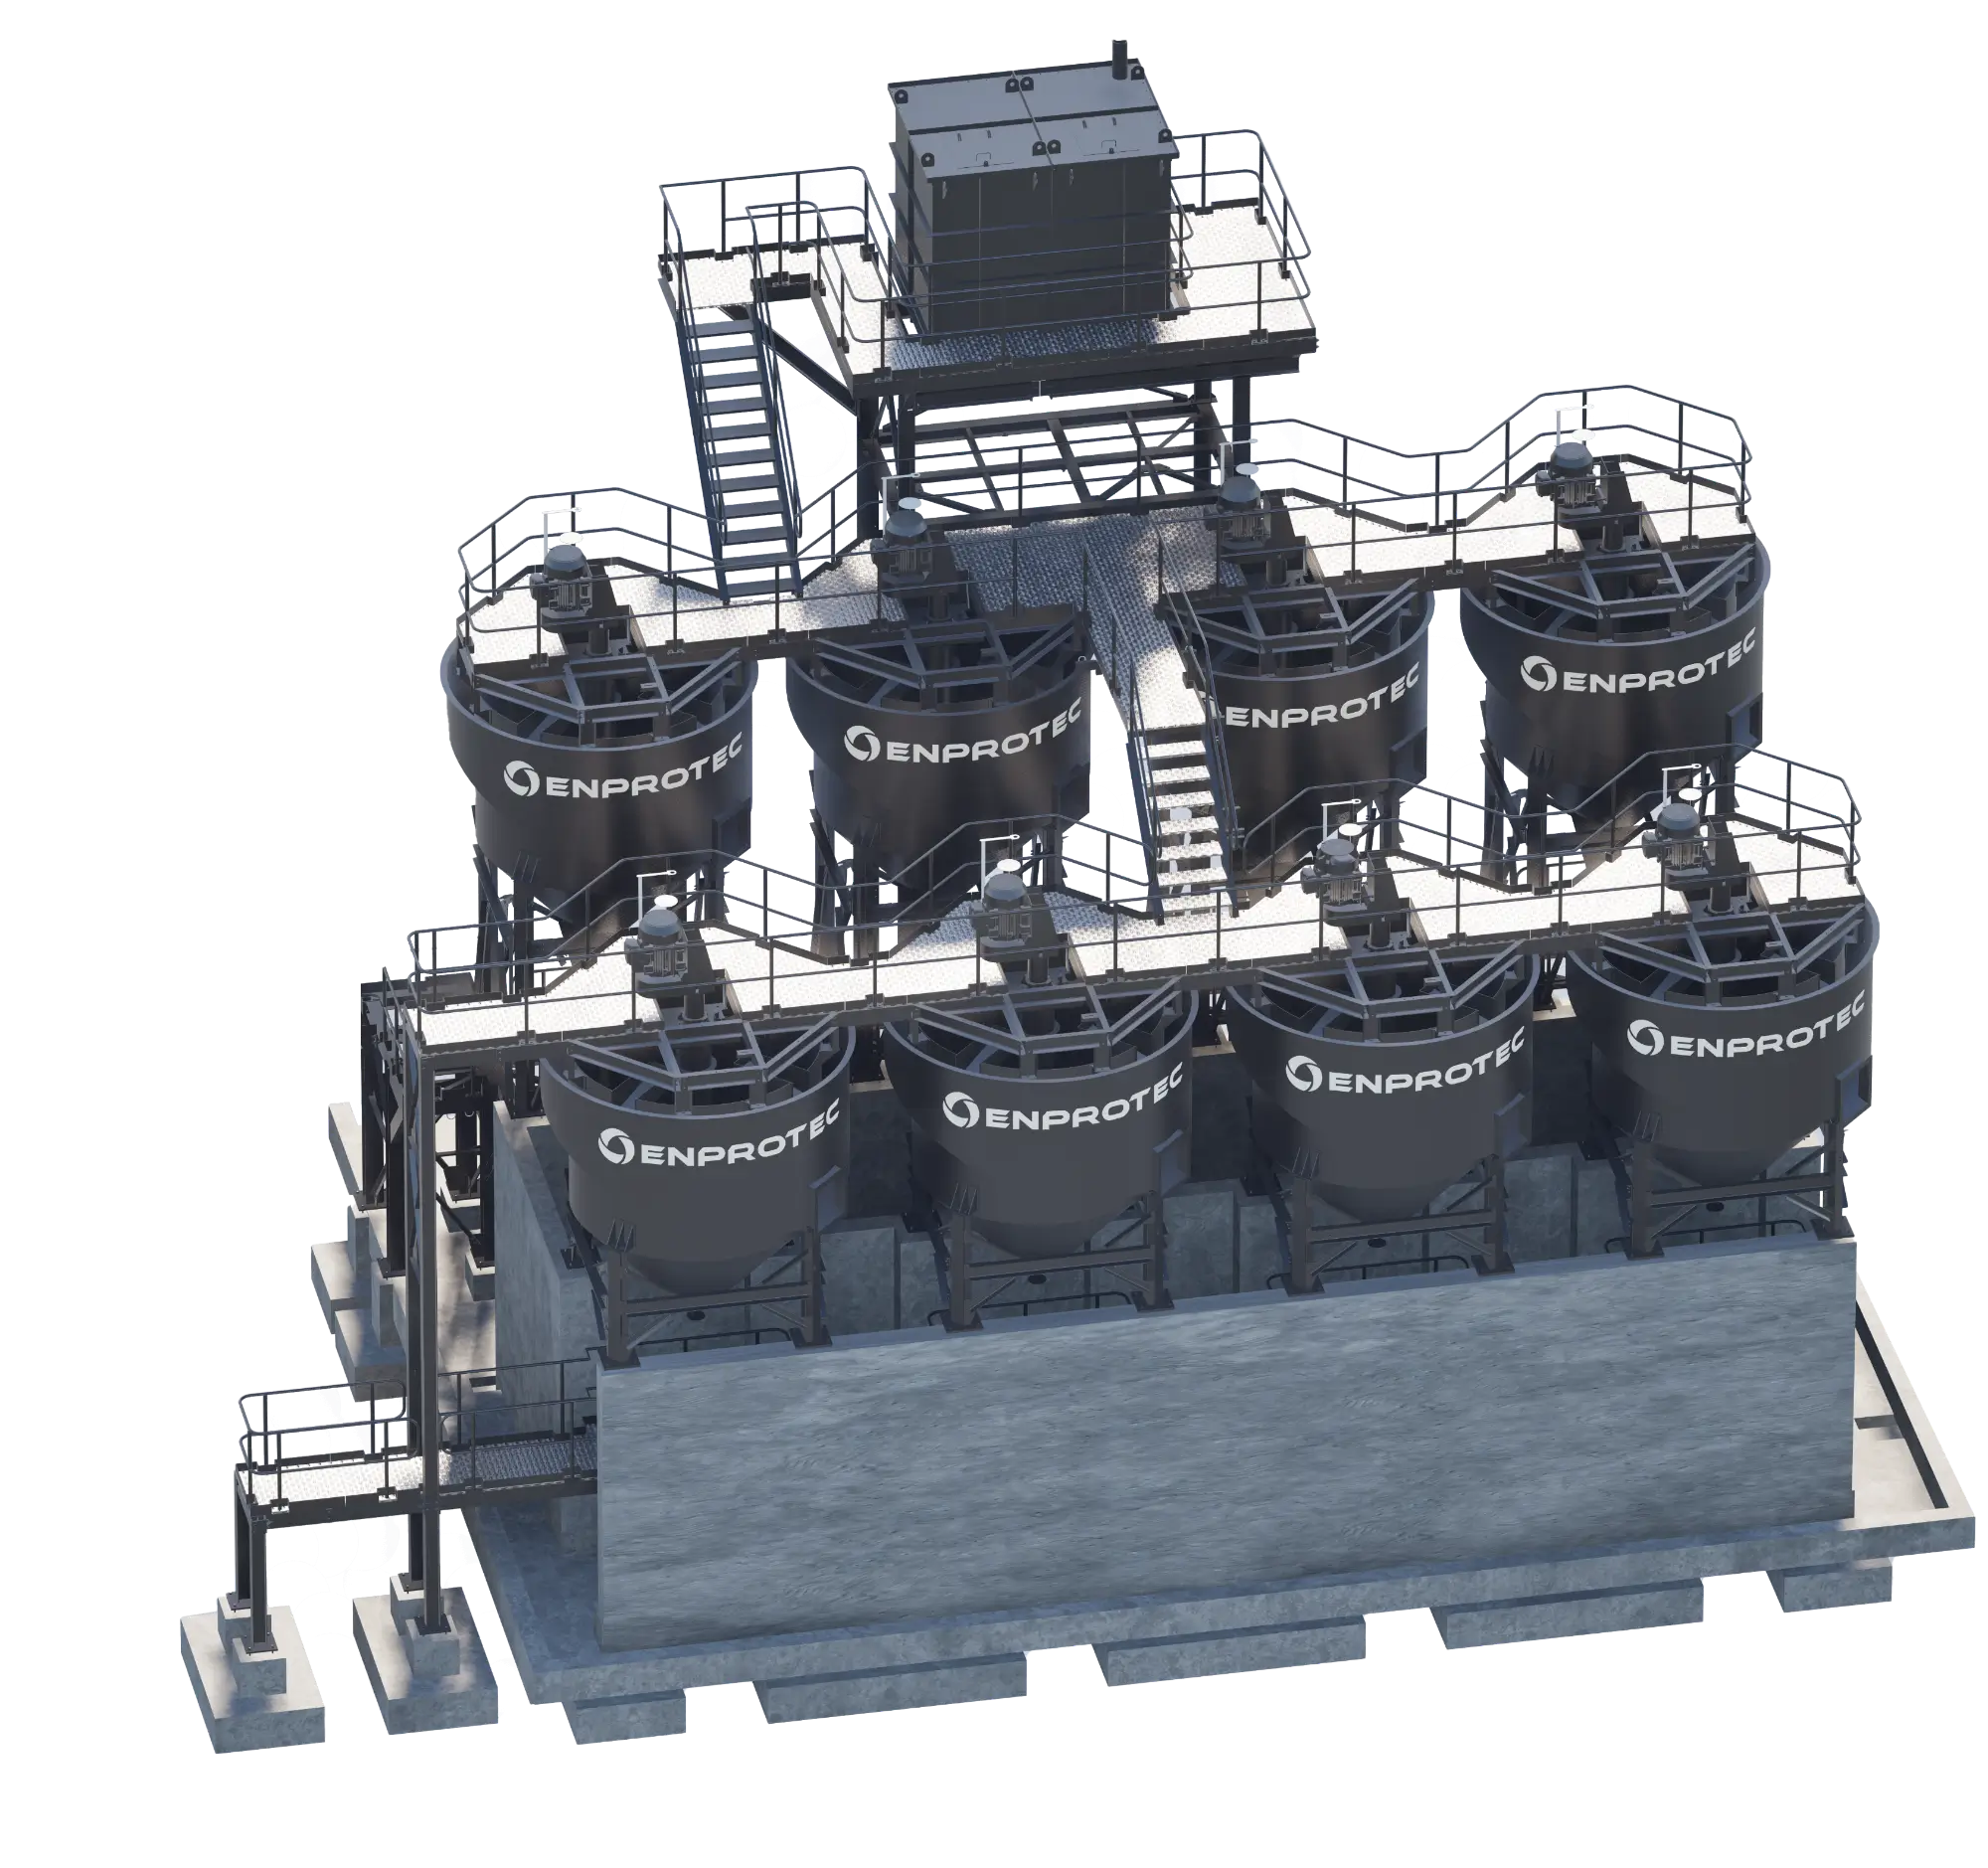
ENPROTEC’s Flotation Technologies are utilised to deliver advanced mineral processing solutions designed to maximise recovery, improve efficiency, and reduce operational costs. Our range of flotation technologies (KinetiCore™, Dual™, Dual Circuit™, MaxFloat™, PneuPure™ and FlashPro™) is engineered to excel across diverse processing requirements for various ore types and plant conditions. Our technologies combine innovative design with robust engineering to ensure superior metallurgical performance and long-term reliability.
By optimising particle-bubble interaction, froth stability, and circuit flexibility, ENPROTEC’s flotation solutions enable higher yields, improved grade control, and reduced energy and reagent consumption. This results in a more efficient, sustainable process that lowers maintenance demands while increasing plant throughput. Whether for fine- or coarse-particle recovery, complex circuits, or ultra-fine applications, ENPROTEC provides tailored solutions that enhance productivity and profitability.
Integrated Reaction Chamber – Localised Energy Input
Our confined, adjustable mechanically agitated reaction chamber forces feed slurry, air and reagents together, resulting in above average energy input, ensuring maximised bubble/particle interaction for efficient flotation kinetics. Additionally, due to the unique efficient energy input, the Dual Cell™ is capable of beneficiating ultra-fine (-25 micron) particles resulting in higher recovery rates in comparison to conventional flotation technology.
Ultra-Fine Bubble Generation
Features & Benefits
- Automated reagent dosage system
- High fractional recovery in ultra fine fractions
- Diverse commodity range and orientations
- Automated froth level control
- Increased concentrate recovery
- High froth carrying capacity
Key Outcomes
- Efficient energy transfer
- Optimised material grades
- Increased recovery of minerals
- Reduced overall operation costs
- Maximised recovery & increased revenue
ENPROTEC Flotation Technologies
KinetiCoreTM Cell
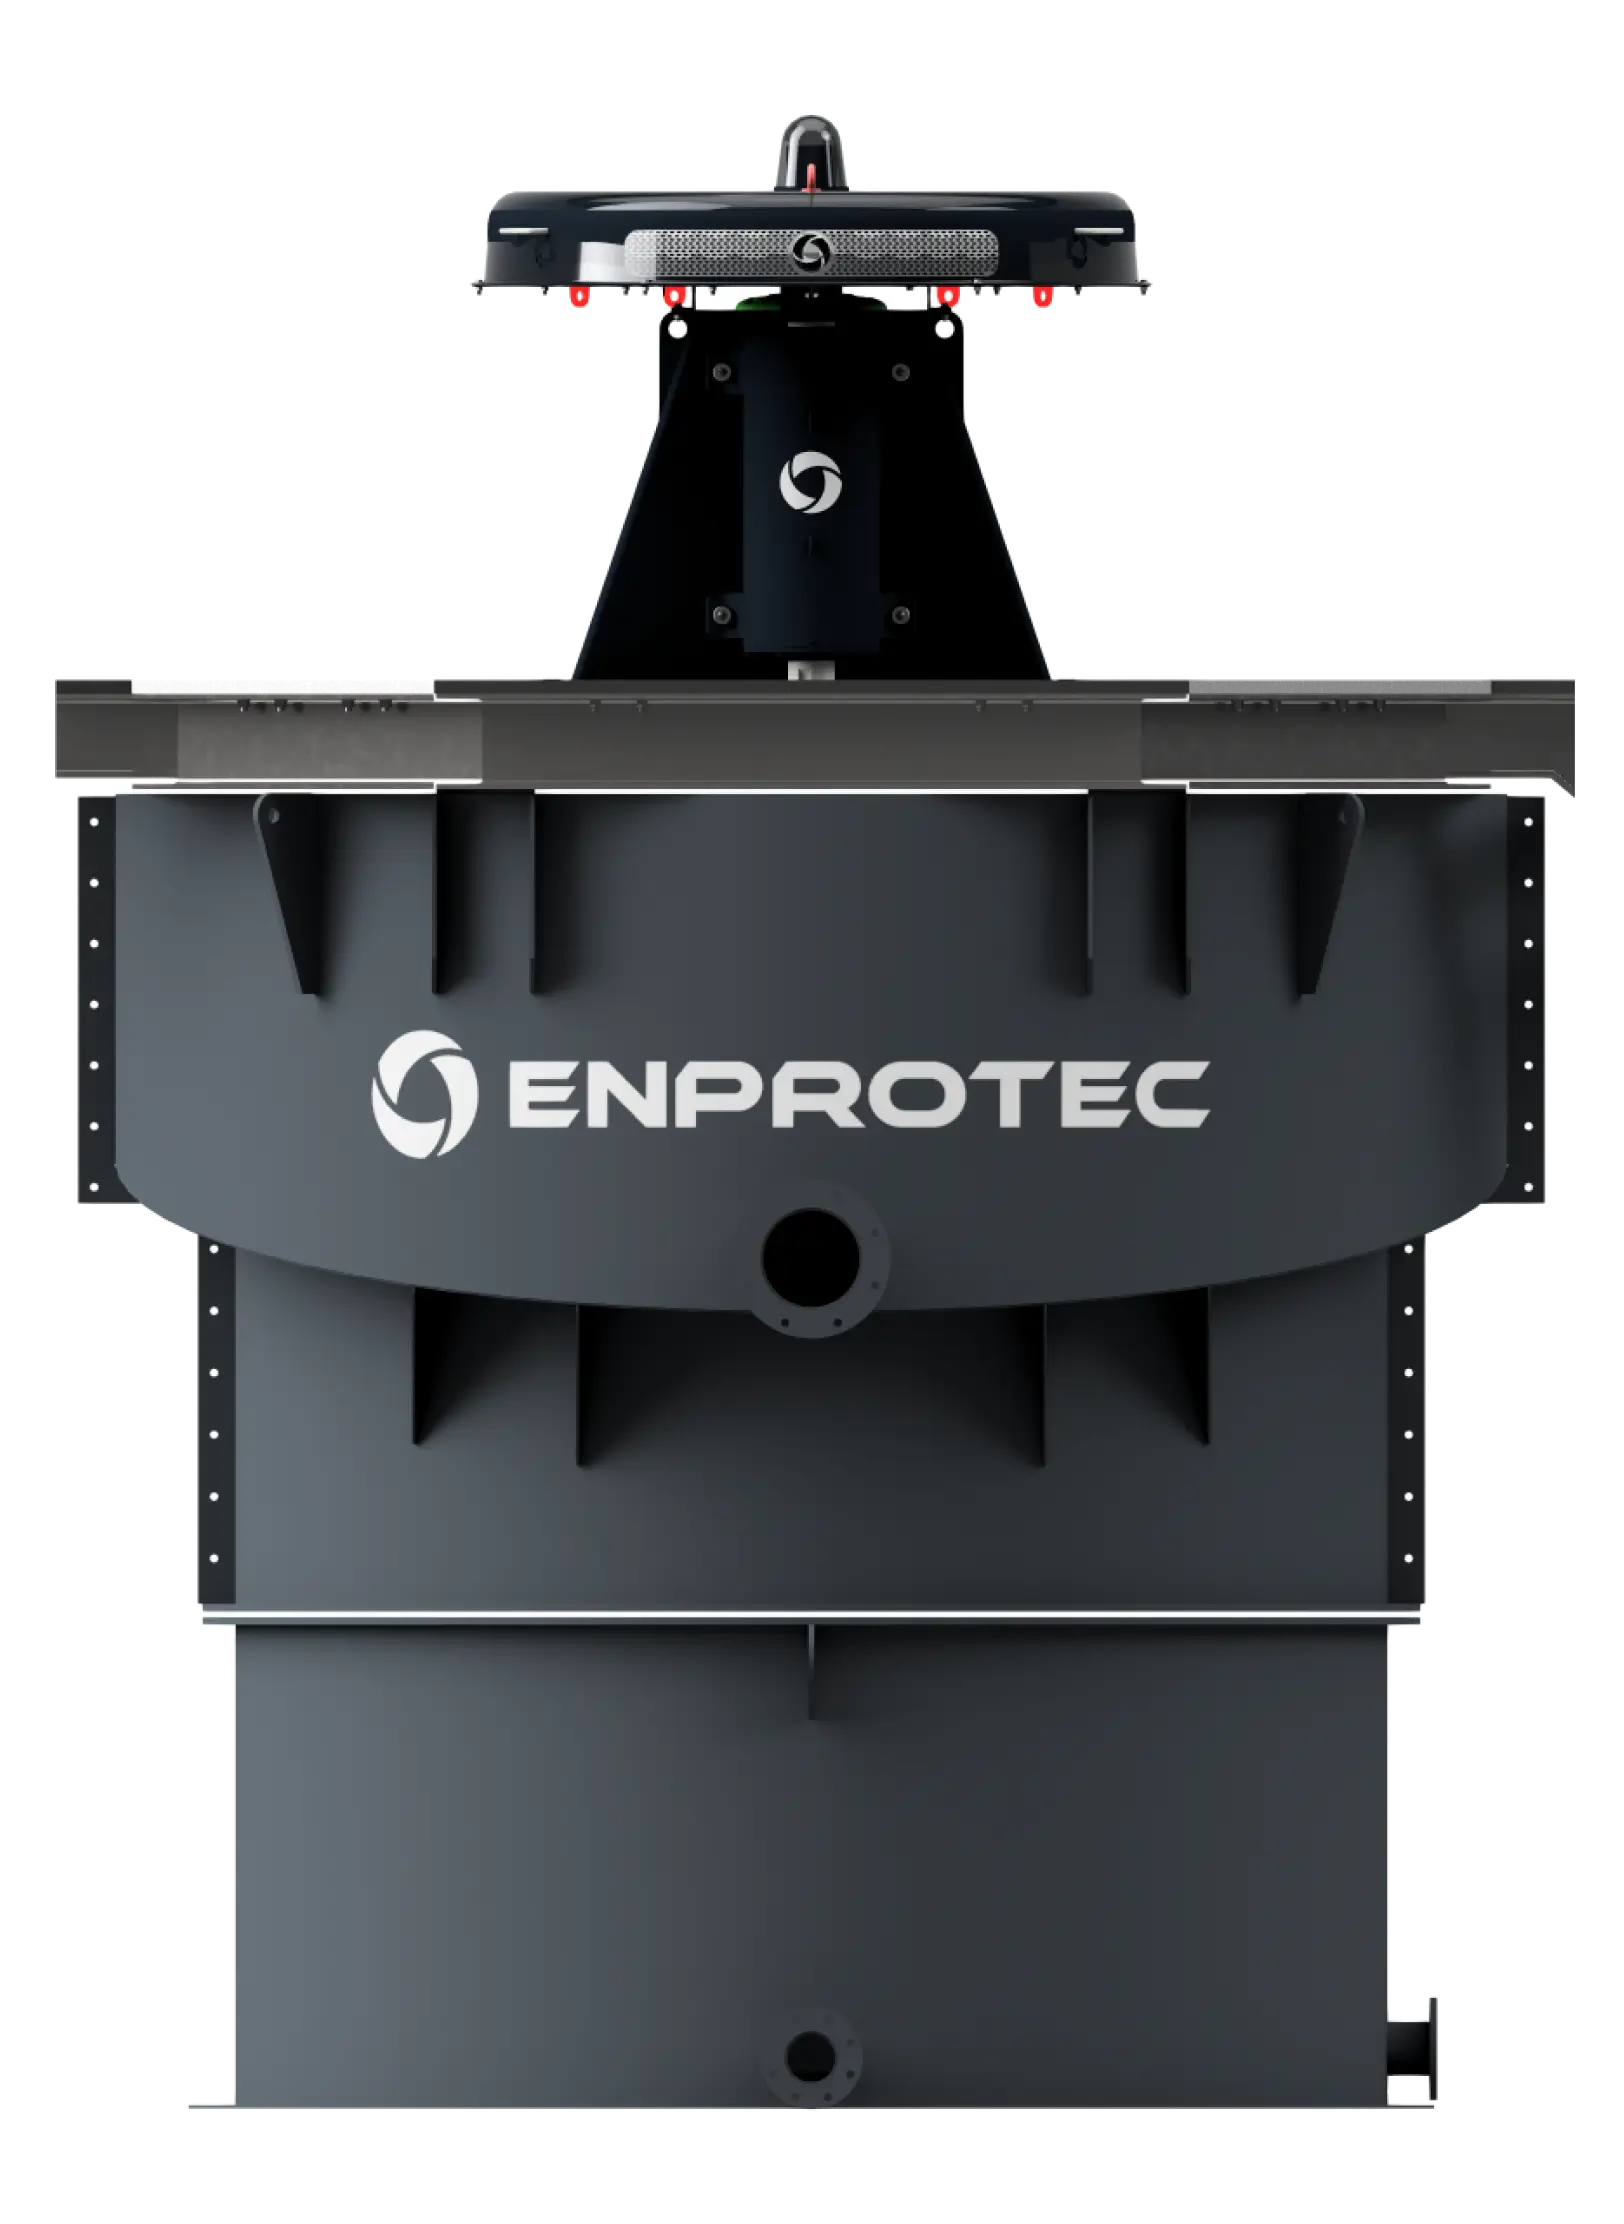
Robust construction for long service life.
Flexible configuration for various ore types.
Enhanced particle suspension for improved recovery.
Consistent performance under varius
throughput conditions
Energy-efficient impeller design reduces operating costs.
Our KinetiCoreTM Cells deliver high-efficiency mechanical flotation through optimised bubble-particle collision and aeration, ensuring superior particle suspension and rapid recovery for diverse mineral processing environments.
Key Applications:
- Recovery of base metal sulphides
- Phosphate ore upgrading
- PGME flotation circuits
- Reverse flotation to remove silica from iron ore
DualTM Cell
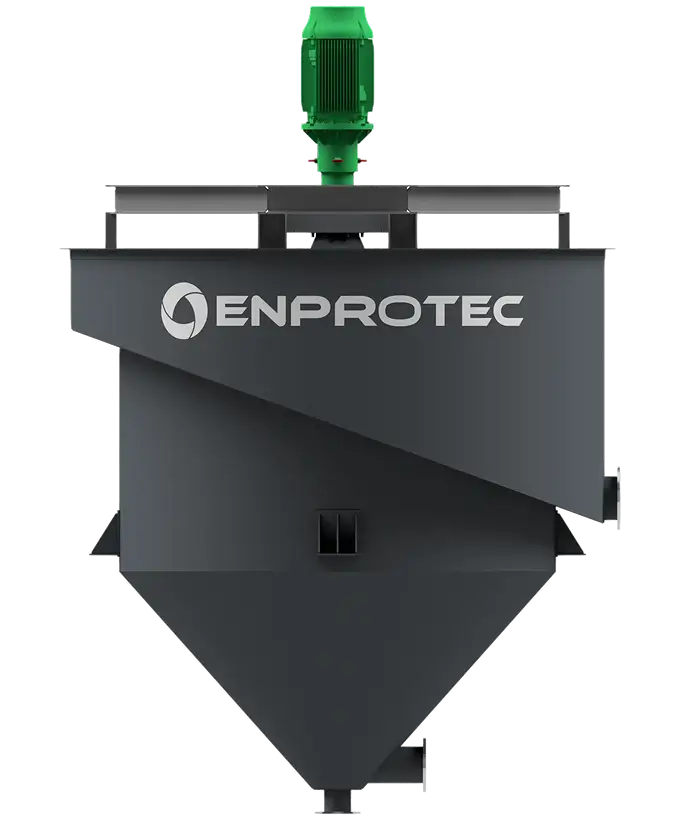
Adaptable to multiple circuit configurations.
Accelerated flotation kinetics for improved recovery.
High energy input for Ultrafine and weathered particle recovery
Compact design for space efficiency.
Durable components for extended operational life.
Our DualTM Cell technology combines intense mixing and aeration for rapid flotation kinetics, enabling high recovery rates in demanding mineral processing environments with complex ore
characteristics.
Key Applications:
- Ultrafine coking coal flotation
- Upgrading of weathered coal ores
- High energy input reaction chamber
- High bubble surface area
- Combined high-shear and low-shear zones in one cell
Dual CircuitTM Cell

Reduced plant footprint and infrastructure costs
Simplified circuit design and maintenance
Improved recovery and grade
Our Dual CircuitTM Cell Optimises energy use and recovery, while reducing footprint and simplifying circuit design for modern mineral processing plants.
Key Applications:
- Ultrafine sulphide flotation applications
- High energy input reaction chamber
- Improved selectivity within <38µm size fractions
- Oxidised sulphide ore flotation applications
- Split lead–zinc circuits with independent chemistry control
- Dual recirculation functionality for stable concentrate quality
- Supplementary reagent dosing system per cell
MaxFloatTM Cell

Superior coarse particle recovery
Optimised air dispersion for improved flotation kinetics
Reduced grinding requirements for energy savings
Low-shear environment minimises particle breakage
High throughput capacity for large-scale operations
Our MaxFloatTM Cells are engineered for coarse particle recovery, combining advanced hydrodynamics and low-shear design to maximise efficiency and reduce losses in challenging flotation environments.
Key Applications:
- Recovery of coarse copper sulfides
- Coarse coal separation after desliming
- Suitable for coarse grained mineral resources
- Reduces material fine grinding requirements
- Reduced overall plant energy consumption
- Flotation of sand-sized tungsten minerals
- Handling feeds with wider particle size distributions
PneuPureTM Cell
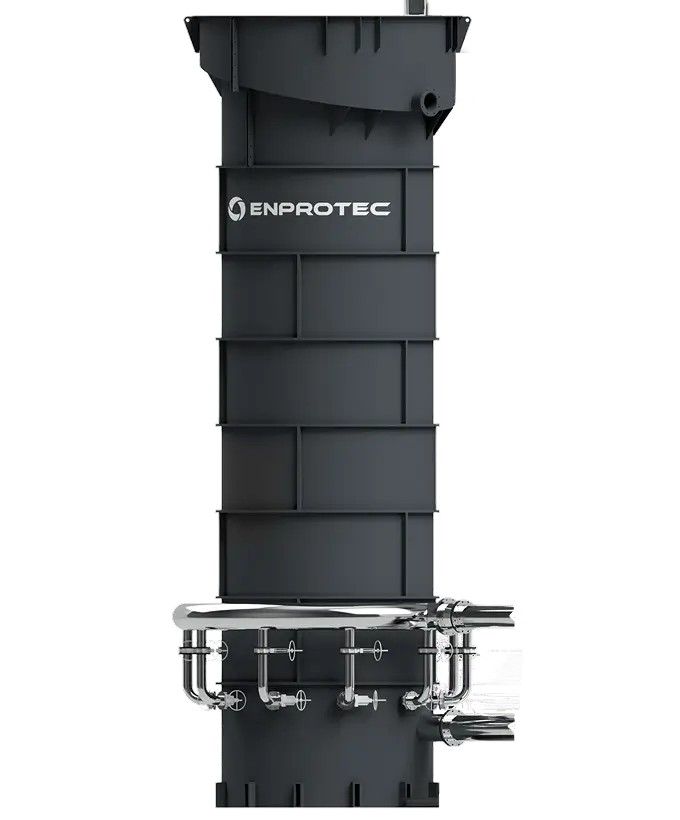
Enhanced froth stability for
consistent performance
High selectivity for fine particle recovery
Improved concentrate grade and purity
Simplified maintenance with
fewer moving parts
Low energy consumption
Our PneuPureTM Cell offers advanced column flotation with pneumatic aeration, delivering exceptional grade control and fine particle recovery for cleaner concentrates and reduced downstream processing costs.
Key Applications:
- Pneumatic flotation technology
- Typical final cleaner stage implementation
- Improved valuable mineral selectivity
- Ultrafine sulfide cleaning with small bubbles
- Deep froth washing to reduce entrainment
FlashProTM Cell
Early recovery of valuable minerals
Reduced circulating load
Compact footprint
Improved overall recovery
Short residence time
Lower energy consumption
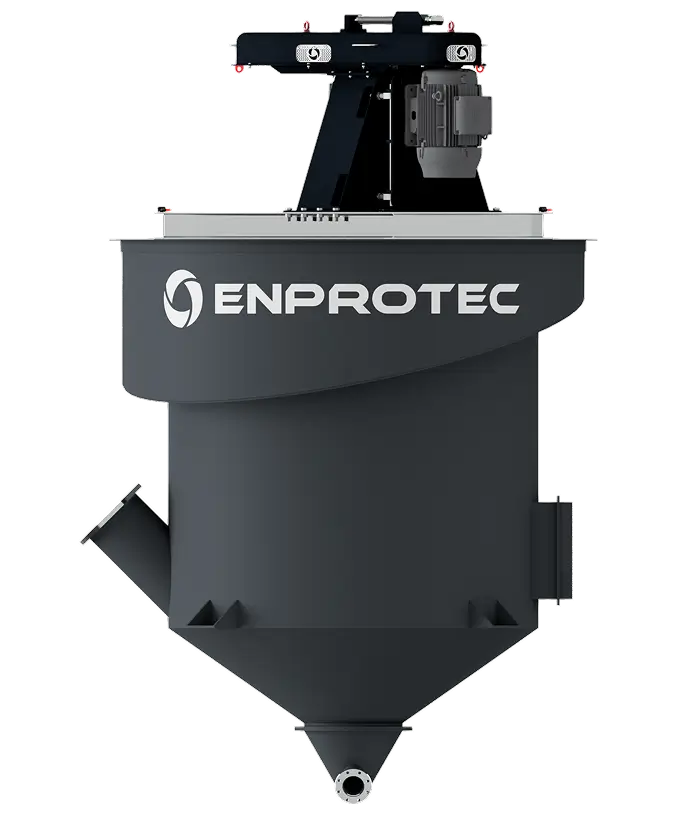
Our FlashProTM cells are inline flotation units, placed between grinding and classification to recover coarse liberated valuables early. High pulp density and short residence time with intense mixing and air dispersion maximise coarse particle recovery. These cells reduce circulating load, eliminate overgrinding, cut energy use and boost plant performance.
Key Applications:
- Recovery of free gold particles from cyclone underflow.
- Coarse particle base metal flotation applications.
- Selective recovery of coarse PGMs.
- Minimises overgrinding of valuable minerals.
- Reduces overall circuit energy consumption.
- Improves recovery in ores with fast-floating mineral fractions.
Technically Engineered
Air Dispersion and Bubble Generation
Effective air dispersion and bubble generation are critical for maximising the flotation cell’s performance. At ENPROTEC, we utilise advanced impeller and diffuser designs that ensure uniform air distribution and ultra-fine bubble creation. This increases the surface area for particle attachment, enhancing the recovery of valuable minerals. The use of high-efficiency air supply systems and precise air control mechanisms further optimises the flotation process, improving separation efficiency and throughput.
Cell Design and Material
The design and material-of-construction of flotation cells impact their durability and efficiency. ENPROTEC employs robust construction materials such as stainless steel and specialised composites that resist corrosion and wear, extending the lifespan of the equipment. Our cell designs, including tank geometry and reaction chamber engineering, are optimised to promote effective mixing and prevent/eliminate short-circuiting, ensuring consistent performance and high recovery rates.
Automation and Control Systems
ENPROTEC flotation technologies are equipped with advanced automation and control systems. These systems utilises PLC, advanced control systems and live analytics to automate and optimise the flotation process, including reagent addition, airflow control, and froth depth management. Real-time monitoring of parameters such as energy input, pH, Eh, and froth depth allows for dynamic adjustments, optimising recovery and grade across a full particle size distribution spectrum. Features like remote monitoring and data logging provide valuable insights for continuous improvement.
Froth Management and Collection
Efficient froth management is essential for maximising recovery and product quality. ENPROTEC’s flotation cells incorporate innovative radial and circumferential froth launders that effectively direct froth to the overflow weirs, minimising froth travel distance, retention time and promoting rapid collection. Adjustable froth washing systems remove entrained gangue particles, improving concentrate grade. Additional options, such as the integration of froth cameras and level sensors, ensure precise control over the froth layer, enhancing operational stability and performance.
FLOTATION TECHNOLOGIES
Further Enhance your Operations
with our Technology
Feed Condition Optimisation
The critical flotation feed parameters, such as feed density, flow rate, pH, Eh, etc., can be optimised to enable an effective flotation process.
Reagent Optimisation
The reagent addition type, dosage, and sequence are crucial for achieving the desired selectivity and recovery rates.
Bubble Size Distribution
Optimising the size and distribution of air bubbles enhances the probability of collision and attachment of hydrophobic particles.
Energy Efficiency
Efficient flotation cells minimise energy consumption through improved cell design, such as optimised reaction chambers and aeration systems.

Creating Better, Greener Mineral Processing
Contact Information
"*" indicates required fields